Whatsapp: +86 18298157670 vicky@yczxairtankdcpump.com

news
What Is a Безмасляный Вакуумный Насос? A Complete Guide to Oil-Free Vacuum Pumps
You are searching for a specific piece of equipment, and the search bar auto-fills something that looks like a glitch: безмасляный вакуумный насос. It’s not a mistake. You are not the only one typing it. As global supply chains bring more international equipment into American labs, dental offices, and workshops, you will keep seeing this Cyrillic phrase stamped on data sheets, manuals, and even the side of the pump itself. But once you cut through the unfamiliar alphabet, you realize the concept is universal. This guide breaks down exactly what a безмасляный вакуумный насос is, how the technology works, and how to pick the right oil-free pump for your work—without getting lost in translation.
Key Takeaways
- Безмасляный вакуумный насос literally translates to “oil-free vacuum pump”—the same technology, just labeled in Russian for a global market.
- Oil-free pumps eliminate contamination risk by removing oil from the pumping chamber, making them ideal for clean applications like labs, dental clinics, and food packaging.
- Diaphragm, scroll, and piston mechanisms each solve different problems; your choice depends on ultimate vacuum, flow rate, and chemical exposure.
- The true cost of ownership often favors oil-free models over five years once you factor in maintenance labor, oil disposal, and energy consumption.
Where the Term Безмасляный Вакуумный Насос Comes From (And Why It Matters)
If you break down the Russian phrase, you get exactly what you expect. Безмасляный (bezmaslyanyy) means “oil-free” or “without oil.” Вакуумный (vakuumnyy) means “vacuum.” Насос (nasos) means “pump.” Put them together, and you have an oil-free vacuum pump—the same device you have been researching in English.
So why are you seeing Cyrillic text in your search results? The short answer is that Russian-language technical literature and manufacturing are deeply integrated into the global vacuum equipment market. Several major manufacturers operate facilities in Eastern Europe, and their technical documentation often carries dual-language labels. You might receive a pump with a nameplate that reads “безмасляный вакуумный насос” right above the English translation. Distributors and resellers list products with both terms to capture international traffic. Your curiosity about the phrase is actually a signal that you are doing thorough research—and knowing this term helps you cross-reference specifications across languages. From a practical standpoint, reading spec sheets in multiple languages can also reveal slight differences in test standards or ratings that matter when you’re trying to hit a specific benchmark, so learning to spot the Cyrillic term gives you an extra layer of due diligence.
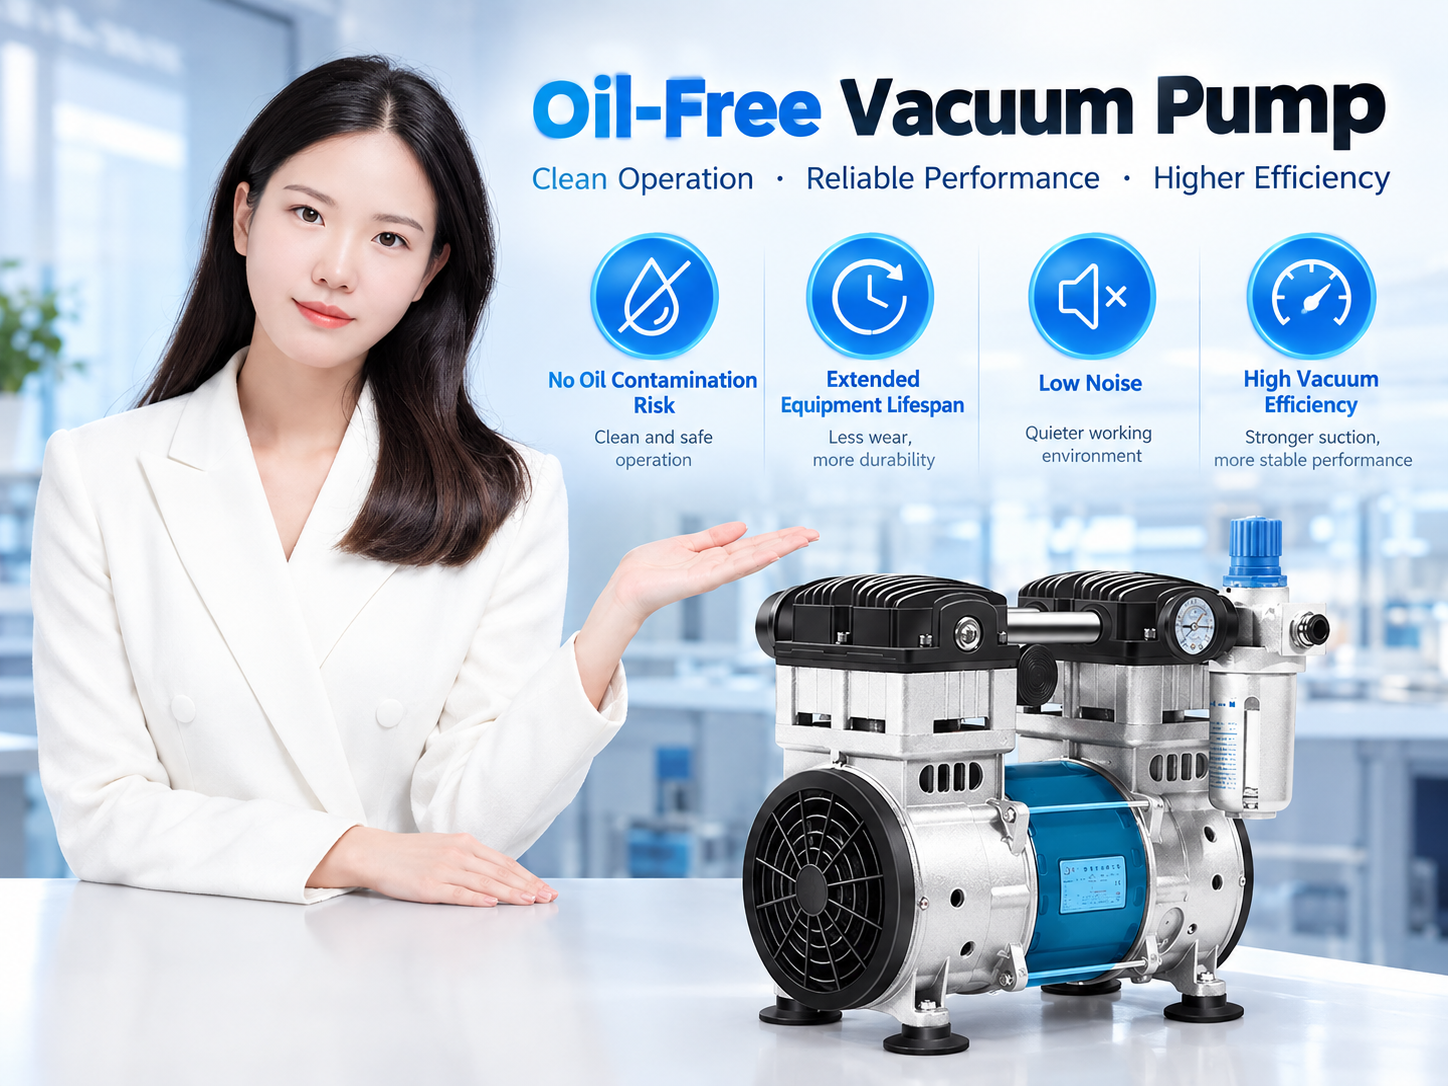
The technology does not change because the alphabet does. An oil-free vacuum pump performs the same function whether it ships from Ohio, Stuttgart, or Chelyabinsk. The critical question is not what language the label uses, but which pumping mechanism inside that housing matches your specific needs.
How an Oil-Free Vacuum Pump Actually Works
You do not need to be a mechanical engineer to grasp the core principle. In a traditional oil-lubricated pump, oil circulates inside the pumping chamber to seal gaps, lubricate moving parts, and carry away heat. The oil touches everything—including the gas you are pulling through the system. In an oil-free pump, the pumping chamber is completely dry. No oil ever contacts the process gas.
Removing oil from the equation sounds simple, but it demands clever engineering. The pump still needs to create a tight seal between moving surfaces and maintain that seal through thousands of operating hours. Three mechanism types dominate the market, and each one solves the sealing problem differently.
Diaphragm pumps use a flexible membrane that flexes up and down. As the diaphragm pulls down, it expands the chamber volume, drawing gas in through an inlet valve. As it pushes up, it compresses the gas and forces it out through an exhaust valve. The diaphragm itself acts as both the moving wall and the seal, so there is no sliding contact between hard surfaces in the gas path. This design also isolates the mechanical drive from the gas stream, which is why you often see diaphragm pumps handling aggressive solvents without degrading the internal bearings.
Scroll pumps use two interleaved spirals—one stationary, one orbiting in a circular motion. Gas enters at the outer edge of the scroll set and gets progressively compressed as the orbiting spiral pushes it toward the center discharge port. The spirals never touch each other; a microscopic gap maintained by precision machining creates a dynamic seal without oil. The engineering tolerance here is incredibly tight: if the gap is too large, the pump loses compression efficiency; too small, and thermal expansion can cause the scrolls to crash. That’s why scroll pumps need careful warm-up and cool-down cycles.
Piston pumps operate on a familiar principle: a piston moves back and forth inside a cylinder, with intake and exhaust valves controlling gas flow. The key difference from your air compressor is the piston ring material. Oil-free piston pumps use self-lubricating materials like PTFE or graphite composites that slide against the cylinder wall without needing liquid lubrication. This simplicity makes them reliable and capable of high flow rates, but the reciprocating action inherently generates more vibration and noise than a rotating scroll or flexing diaphragm.
At a glance: In an oil-lubricated pump, you are deliberately mixing oil with your process. In an oil-free pump, you keep the process gas completely isolated from any lubricant. That single difference cascades into every advantage and limitation you need to evaluate.
Oil-Free vs. Oil-Lubricated Vacuum Pumps: Honest Pros and Cons
No single pump technology wins every matchup. Your decision should hinge on what you are pumping, how deep a vacuum you need, and what you are willing to tolerate in terms of noise, maintenance, and upfront cost. Here is the balanced comparison.
Contamination Risk and Clean Applications
The defining advantage of an oil-free pump is zero contamination risk from pump oil. In an oil-lubricated rotary vane pump, a fine oil mist inevitably backstreams into your vacuum chamber—especially during roughing and cycling. For a lab running vacuum filtration with sensitive samples, that mist contaminates your filter membrane and skews results. For a dental clinic evacuating saliva and debris, oil mist creates a mess. For a food packaging line, oil contamination means rejected product.
Oil-free pumps eliminate this problem entirely. The pumping chamber contains nothing but the gas you are moving. This makes them the default choice for cleanroom applications, analytical instruments, medical suction, and any process where purity matters.
The tradeoff comes in ultimate vacuum. A quality two-stage oil-sealed rotary vane pump can reach ultimate pressures around 0.001 Torr (1.3 Pa). In contrast, diaphragm pumps typically bottom out around 0.5–1.5 Torr, scroll pumps around 0.01–0.05 Torr, and oil-free piston pumps around 0.1–0.5 Torr. If your application requires high vacuum below the 0.01 Torr range, you will likely need an oil-lubricated pump or a more complex oil-free system with multiple stages.
Maintenance, Noise, and Upfront Cost
Oil-free pumps generally cost more to buy and less to own. The initial purchase price for a scroll pump or a high-quality diaphragm pump runs 20–50% higher than an equivalent oil-lubricated rotary vane pump. But you eliminate the recurring costs of oil changes, oil filters, and disposal fees. You also eliminate the labor hours your team spends draining, refilling, and cleaning up oil spills.
A common mistake is to dismiss noise as a minor annoyance rather than a real operational variable. In a bustling lab, a pump that hums at 62 dBA may blend into the background. But place that same pump in a quiet dental operatory or a classroom where precision work happens inches away, and it becomes a distraction that affects concentration and even patient comfort. Always match the pump’s noise profile to your actual working distance. If you’re setting up a benchtop system in a shared space, ask your supplier if they have a demo unit you can listen to before buying—decibel charts only tell part of the story.
Noise is a real and often overlooked factor. Here are typical sound pressure levels measured at one meter:
| Pump Type | Typical Noise Level (dBA) |
|---|---|
| Oil-lubricated rotary vane | 48–62 |
| Diaphragm pump | 45–55 |
| Scroll pump | 52–60 |
| Oil-free piston | 55–68 |
Diaphragm pumps tend to run the quietest, which makes them popular in benchtop lab settings where you are working right next to the pump. Piston pumps can be noticeably louder—comparable to a small air compressor cycling on and off. The underlying reason is physics: a reciprocating piston creates pressure pulsations that transmit through the cylinder walls and into the air, while a smooth orbiting scroll or flexing diaphragm generates much less mechanical impact. If your workspace has noise constraints, check the manufacturer’s published decibel rating before you buy.
Maintenance intervals tell a different story for each type. Oil-lubricated pumps need oil changes every 500–2,000 hours depending on duty cycle and contamination load. Diaphragm pumps typically need diaphragm and valve replacements every 10,000–15,000 hours. Scroll pumps require tip seal replacement at similar intervals. Oil-free piston pumps may need ring and cylinder service periodically, though less frequently than oil changes on a rotary vane pump. One mistake new users make is assuming that “oil-free” means “service-free” and ignoring the manufacturer’s recommended intervals entirely. This isn’t a set-it-and-forget-it purchase—each design has wear parts that demand scheduled attention. Skipping those intervals shortens the pump’s life and often leads to sudden failure at the worst possible time, like mid-filtration during a critical experiment.
Choosing the Right Oil-Free Vacuum Pump for Your Application
You now know the mechanism types and tradeoffs. The next step is matching a specific pump to your actual work. Focus on three specifications first: ultimate vacuum, flow rate, and chemical compatibility.
Key Specifications to Prioritize
Ultimate vacuum is the deepest pressure the pump can achieve with the inlet blocked. This number tells you whether the pump can physically pull down to the level your process demands. For vacuum filtration in a lab, 0.5–1.5 Torr from a diaphragm pump is usually sufficient. For rotary evaporation or vacuum ovens, you may need the 0.01–0.05 Torr range that a scroll pump provides. For roughing a turbo pump, an oil-free scroll or multi-stage diaphragm pump works well.
Flow rate, typically measured in CFM or L/min, determines how fast the pump evacuates your chamber. A pump with excellent ultimate vacuum but tiny flow rate will take forever to pull down a large volume. For a dental vacuum system with multiple operatories, you might need 2–4 CFM or more. For a small benchtop desiccator, 0.5–1 CFM is plenty. Match the flow rate to your chamber size and desired pump-down time.
Chemical resistance matters if you are pulling anything other than clean, dry air. Solvent vapors, acid fumes, and moisture all attack pump internals. Diaphragm pumps with PTFE-coated heads and Kalrez or FFKM valves handle aggressive chemicals well. Scroll pumps can tolerate some vapors but struggle with condensable or corrosive gases unless equipped with a gas ballast or purge. Piston pumps generally do not like chemical exposure at all—they are best for clean air applications.
The single most expensive error you can make when selecting an oil-free pump is ignoring the chemical composition of your process gas. I have seen a lab switch from oil-lubricated to diaphragm pumps to avoid contamination, only to order standard neoprene diaphragm heads. Within weeks, acetone vapors swelled the neoprene until the diaphragms failed. The fix was straightforward—PTFE-coated heads—but the downtime and the replacement cost taught an expensive lesson. Before you buy, list every solvent, acid, or reactive gas your vacuum line will ever see, and then verify that the materials in the pump head, valves, and seals are compatible with each one. Most manufacturers publish chemical resistance charts; if they don’t, ask for one.
Matching Pump Type to Industry
Laboratory: diaphragm or scroll. Diaphragm pumps dominate benchtop applications like filtration, solid-phase extraction, and gel drying. Scroll pumps step in when you need deeper vacuum for Schlenk lines, centrifuges, or backing turbomolecular pumps.
Dental and medical: oil-free piston or diaphragm. Dental clinics need reliable, continuous suction. Oil-free piston pumps handle this well and tolerate occasional liquid carryover better than scroll pumps. Diaphragm pumps work for smaller suction units and portable aspirators.
Industrial and packaging: scroll or multi-stage diaphragm. Food packaging, pick-and-place automation, and printing equipment use vacuum extensively. Scroll pumps offer a good balance of flow rate and depth. Diaphragm pumps work where contamination risk is the top concern.
Hobby and small workshop: diaphragm. If you are degassing resins, stabilizing wood, or running a small vacuum chamber, a single-stage diaphragm pump is affordable, quiet, and forgiving.
Imagine this real-world scenario: You’re running a small analytical service lab. A client sends fifteen water samples for suspended-solids analysis using vacuum filtration. Your old oil-lubricated pump starts blowing a faint white mist from the exhaust just as you’re setting up, and you can see a tiny oil film beginning to form on the filter holder. You realize that the very device meant to pull clean water through the membrane is now a source of contamination. You swap in a diaphragm pump and run the full batch without a single artifact. The relief is immediate, and you avoid having to repeat the work or explain a contaminated blank to the client. That single switch justifies the oil-free investment in a morning’s work.
Calculating the True Cost of Ownership Over 5 Years
The price tag on the website is just the entry fee. What you really pay over five years includes electricity, consumables, and the labor hours your team spends keeping the pump running. Here is a straightforward formula you can use:
Total 5-Year Cost = Purchase Price + (Watts × Hours per Year × 5 × Electricity Rate) + (Annual Maintenance Parts × 5) + (Labor Hours per Year × Labor Rate × 5)
Let’s run an example scenario for a typical US lab. You are choosing between a $1,500 oil-lubricated rotary vane pump and a $2,200 scroll pump, both delivering about 1.5 CFM. The lab operates the pump 2,000 hours per year at an electricity rate of $0.12 per kWh. Your technician’s labor rate is $35 per hour.
Oil-lubricated pump scenario:
- Purchase price: $1,500
- Power: 250 watts → $60/year in electricity → $300 over 5 years
- Oil changes every 1,000 hours: 2 changes/year × $30 in oil and filters = $300 over 5 years
- Labor: 1 hour per oil change × 2 changes/year × $35 = $350 over 5 years
- Disposal fees: $20/year → $100 over 5 years
- Total 5-year cost: $2,550
Oil-free scroll pump scenario:
- Purchase price: $2,200
- Power: 200 watts → $48/year in electricity → $240 over 5 years
- Tip seal replacement at 15,000 hours: one replacement in year 4, $200 in parts
- Labor: one 2-hour service × $35 = $70
- No oil, no disposal
- Total 5-year cost: $2,710
In this example, the numbers come out close. But change the variables—more operating hours, higher labor rates, frequent contamination requiring early oil changes—and the oil-free pump pulls ahead. In a dental practice running 3,000 hours per year with a $50/hour technician rate, the oil-free option typically saves $400–$800 over five years. The crossover point where oil-free becomes cheaper depends on your specific duty cycle and labor costs, but for many high-usage scenarios, the math favors going oil-free.
A hidden cost many first-time buyers forget to include is the time spent cleaning up oil mist from surfaces around the pump or dealing with occasional spills. Even if the pump itself works perfectly, a rotary vane pump in a tight space almost always leaves a thin film on nearby shelves or equipment, and removing it takes real effort. Oil-free pumps don’t have this problem, which adds another qualitative saving that rarely shows up in a spreadsheet but matters when you’re the one with the cleaning rag.
Maintenance Myths and Realities for Oil-Free Pumps
You have probably seen “maintenance-free” in marketing copy for oil-free vacuum pumps. The phrase is misleading. No mechanical device with moving parts is truly maintenance-free. What the manufacturer means is “no oil changes required”—which is accurate and valuable, but it is not the whole story.
Diaphragm pumps need diaphragm and valve replacement on a schedule. A diaphragm flexes millions of times over its life and eventually fatigues. Most manufacturers specify replacement at 10,000–15,000 operating hours. The job typically takes under an hour with basic tools. Ignoring the interval means you eventually lose vacuum performance or risk a diaphragm rupture that contaminates the pump head.
Scroll pump tip seals wear predictably. The tip seals on the orbiting scroll maintain the critical sealing gap. They wear down gradually, and you will notice your ultimate vacuum slowly degrading when they need replacement. This is normal and expected, not a failure.
Clean inlet filters are not optional. An oil-free pump has tight clearances. Particulate debris entering the inlet can score surfaces, jam valves, and accelerate wear catastrophically. Use an inlet filter rated for the particle size you expect, and check it regularly. A $5 filter element saves a $500 repair.
A real-world example of what happens when you ignore the filter: A university lab was using a diaphragm pump to evacuate a small drying oven that held soil samples. Fine dust from the soil inevitably drifted toward the vacuum port. The operators never checked the inlet filter because “the pump is maintenance-free.” After eight months, the filter clogged completely, the pump began running hot, and the diaphragm eventually tore from the extra strain. The repair cost several hundred dollars and caused two weeks of downtime. A weekly glance at the filter element and a $10 replacement would have prevented the whole episode.
Signs of wear that demand attention include longer pump-down times, failure to reach expected ultimate vacuum, unusual vibration or knocking sounds, and visible particulate in the exhaust. Catching these early lets you plan service during scheduled downtime rather than reacting to a failure in the middle of a run.
0users like this.